

Production Optimisation: Create Lasting Results in 2026

Production is running. Orders are coming in. People are busy. Yet, momentum is lost in minor stoppages, unclear handovers, a lack of standards and the same mistake recurring on a new shift. This is the situation many find themselves in right now. Not a factory in obvious crisis, but an operation that never quite reaches its actual potential.
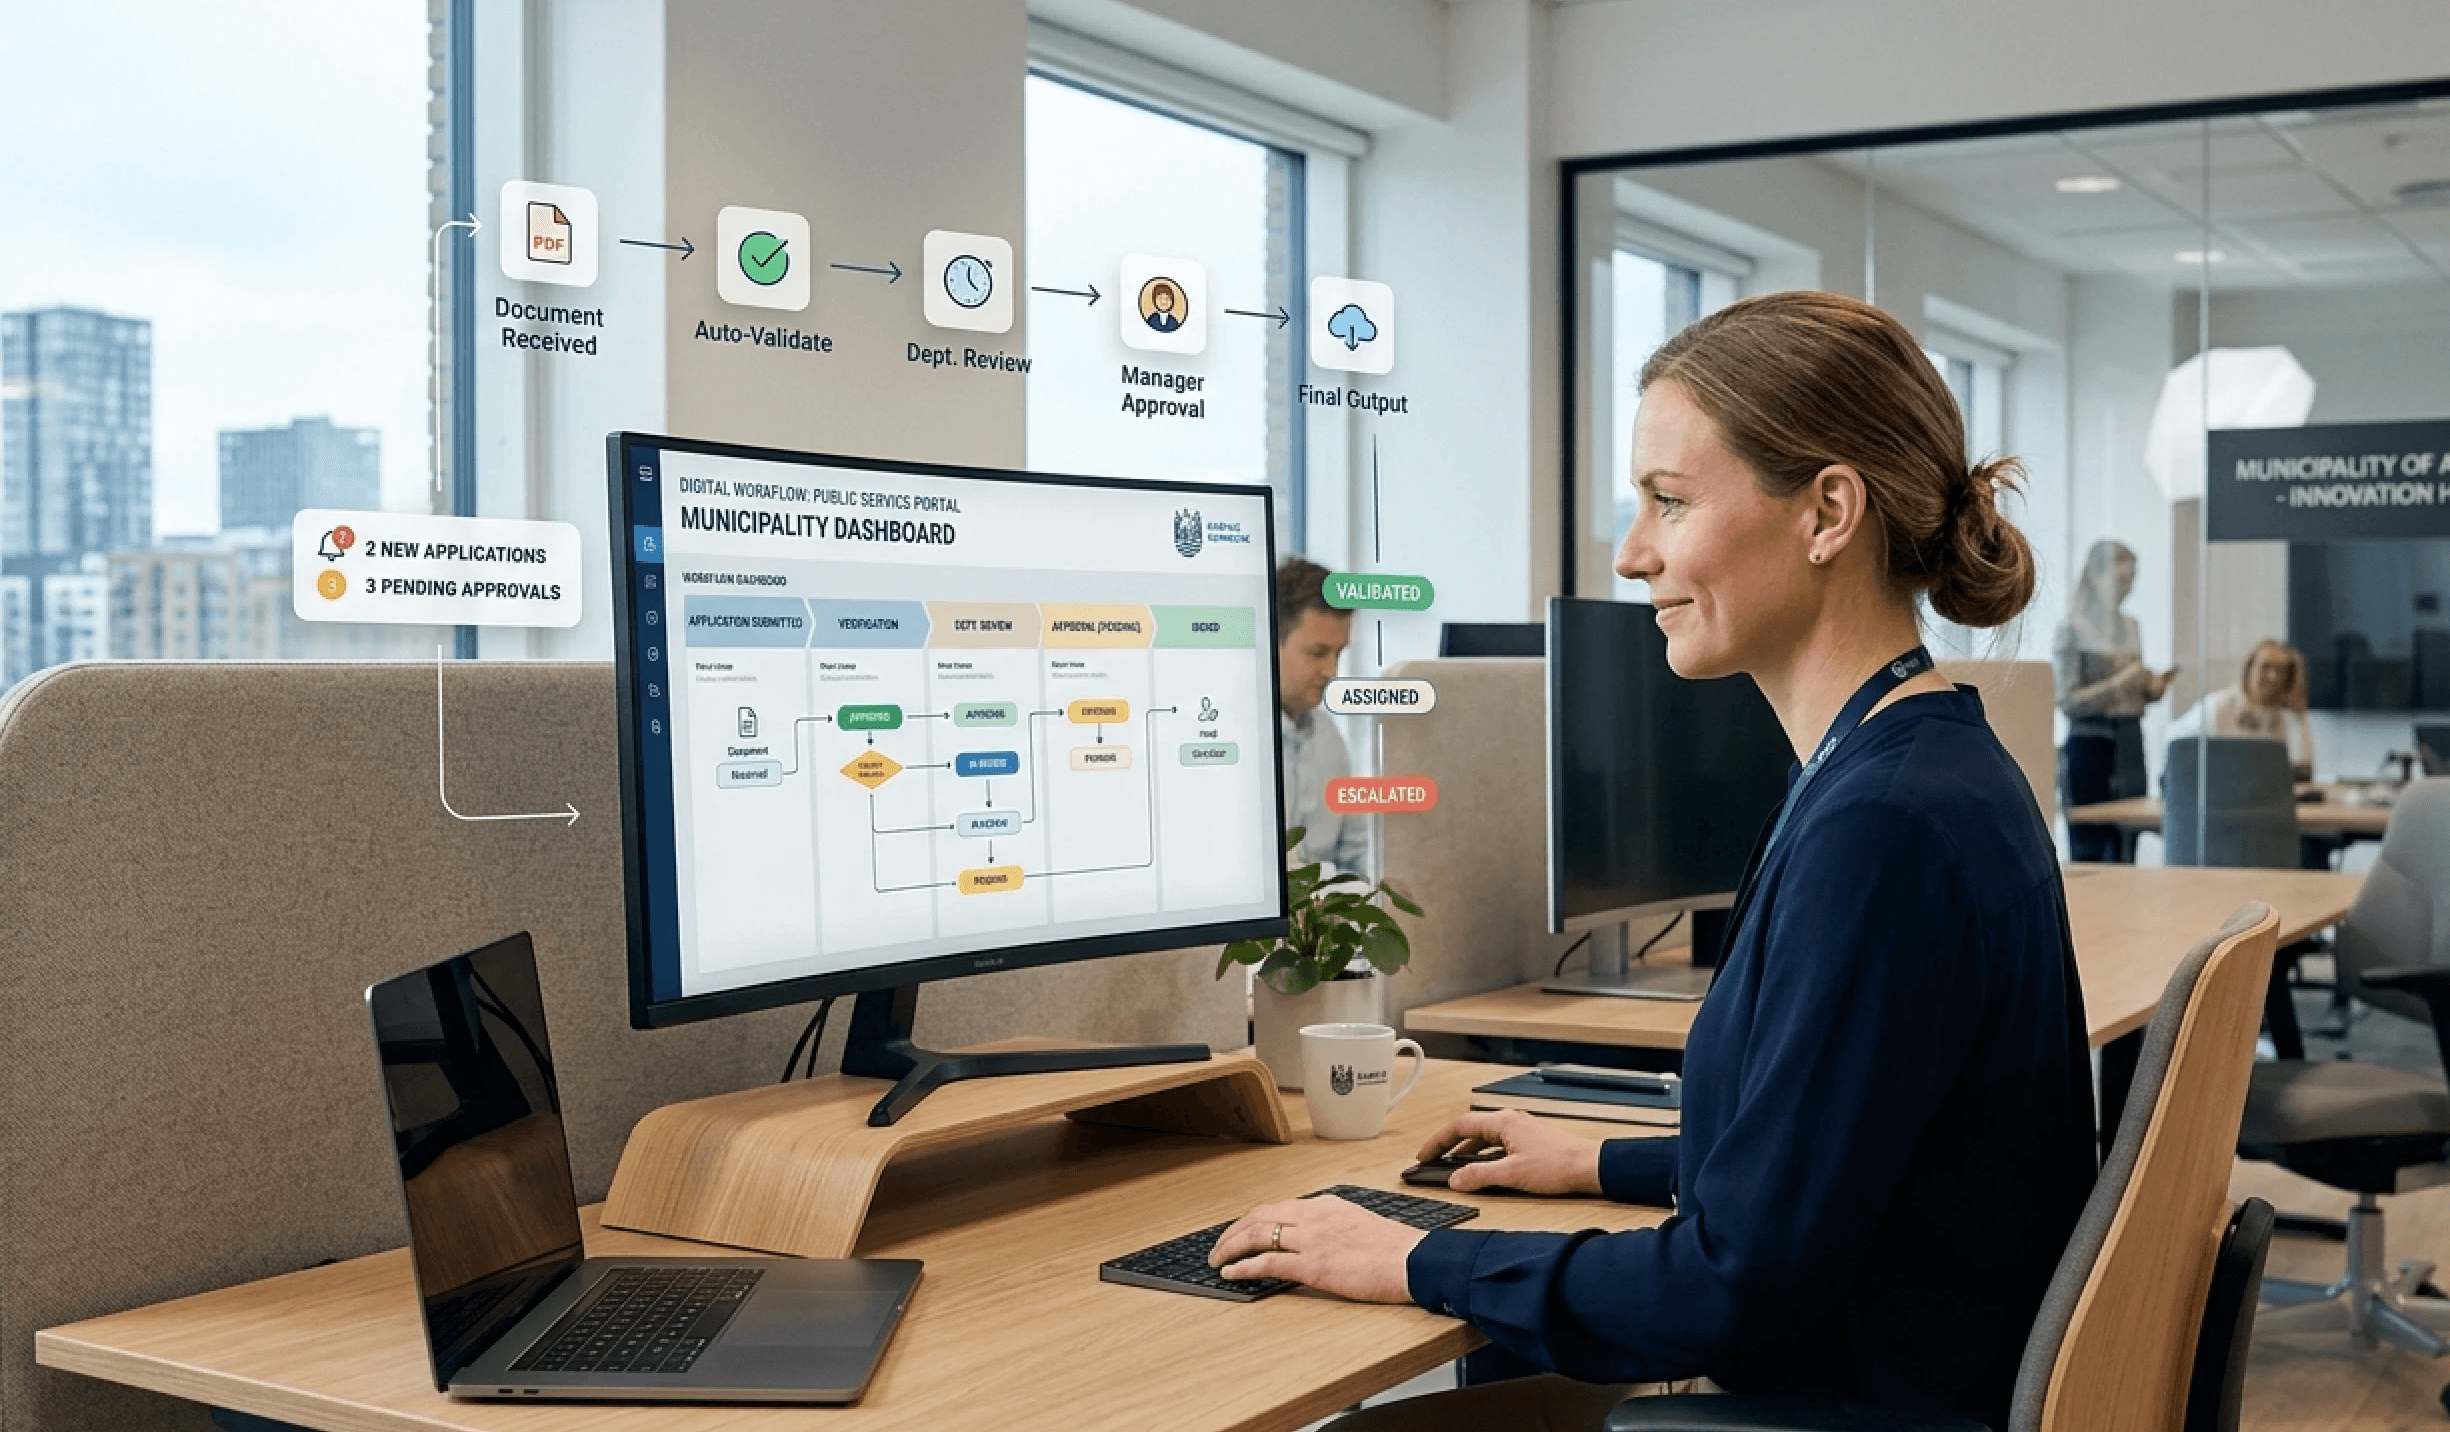
This is where production optimisation becomes interesting. Not as a project with fancy slides, but as systematic work with flow, quality, maintenance, communication and access to knowledge. The classic methods still work. Lean, Six Sigma and TPM have not become obsolete. What is often missing is the digital infrastructure that makes the methods live in the daily routine across shifts, lines and locations.
Why production optimisation is more than just cost savings
Many reduce production optimisation to a single question: How can the company produce more cheaply? This is too narrow. When done properly, optimisation is just as much about creating stable operations, fewer errors, more peace of mind on the floor and better decisions close to the process.
A line with many small interruptions often looks acceptable from the outside. The machines are running. People are working. But below the surface, losses lie in waiting times, changeovers, rework, chasing information and the classic situation where the operator knows what should be done but does not have the same version of the instruction as the technician or planner. This is not just a process problem. It is a communication problem.
Production often fails in the handover
Most factories already have familiar methods on the shelf. They have huddle meetings, SOPs, improvement forms and perhaps a Lean board in the hall. Yet, initiatives lose momentum because knowledge is scattered. Some is in Excel. Some is in folders. Some exists only with specific key personnel. Some is mentioned at a morning meeting and is gone again after lunch.
Even the best improvement plan dies quickly if employees cannot find the latest standard or see why the change was made.
Therefore, modern production optimisation is not only a question of machines, layout and capacity. It is also a question of how the company organises its shared knowledge and daily communication. A shared digital foundation makes the difference between an initiative that remains local and an improvement that becomes standard.
For companies working with production and digital cohesion, the point is simple. If improvements are to stick, they must be easy to find, easy to understand and easy to use in operations.
The right goal is a more robust flow
When production managers succeed with optimisation, three things typically happen simultaneously:
The flow becomes more stable. Fewer unforeseen stoppages and fewer manual workarounds occur.
Quality becomes easier to control. Deviations are detected earlier, and reactions become more consistent.
Work becomes less dependent on individuals. Knowledge moves from heads and piles of paper to shared practice.
This is also why pure cost-cutting projects so often disappoint. If the company only chases lower costs, it often pushes the pace up without resolving the root causes of the losses. The result is more fire-fighting, not better operations.
How to find hidden waste in production
Waste rarely hides in large, dramatic incidents. It lies in the repetitive tasks that everyone has grown accustomed to. A pallet that needs to be moved twice. An operator waiting for release. A quality deviation that is passed on because the next stage "usually" catches it. Therefore, the hunt for waste must begin out in the process and not in a meeting room.
Go where the work happens
A good Gemba walk is not a tour with quick opinions. It is a disciplined observation. The manager or improvement team follows the material, observes the movements, notes interruptions and asks about what the employees are actually experiencing.
The questions must be concrete:
Where does the work typically wait? Between which steps does a queue form, and what triggers it.
What forces people to improvise? Is there a lack of tools, materials, instructions or decisions.
Where does rework occur? Not just defects that are discarded, but also everything that is corrected, adjusted or checked an extra time.
What shifts between teams? If the process runs differently from morning to evening, the standard is likely unclear or not anchored.
The crucial thing is to observe without immediately proposing solutions. Many overlook waste because they move too quickly to improvement tools. First, the problem must be seen in its true context.
Practical rule: Follow one order, one batch or one unit all the way through. This often reveals more than an hour of general talk about "challenges in production".
Building, logistics and maintenance also play a bigger role than many admit. Poor access routes, unclear material flows and a lack of structure around service tasks create hidden losses every day. Therefore, it can be useful to look at how others work with strategic property management and maintenance as part of overall operational thinking.
Look for patterns, not single events
One bad day is not necessarily a problem. A repeated pattern is. Therefore, observations must be linked with simple operational data, the shift's experiences and concrete daily occurrences. Not to conduct heavy analyses from the start, but to distinguish between noise and real opportunities for improvement.
A practical approach is to work with three categories on the floor:
Focus area | What is typically seen | What it often points to |
|---|---|---|
Material flow | Unnecessary transport, intermediate storage, searching for components | Layout problem or weak planning |
Process flow | Waiting time, changeovers, unclear releases | Lack of standard or poor coordination |
Information flow | Varying instructions, oral special rules, delayed messages | Weak knowledge sharing and unclear communication |
This simple exercise works because it makes problems visible without drowning the team in theory. Operators, technicians and managers can quickly see where they are losing time and why it is happening.
What does not work is running a single workshop, filling out a waste types chart and believing that you now understand the process. Waste is found in work, not in PowerPoint.
Choose the right method and tools
Once problems are visible, the next classic misstep occurs. The company chooses a method because it is popular, not because it fits the task. Lean, Six Sigma and TPM do not solve the same problems. They can be combined, but they should not be mixed together without direction.
Before comparing, it makes sense to see the methods in a simple overview.
When Lean makes the most sense
Lean is the strongest choice when the company struggles with flow, unnecessary steps, long lead times or a production where materials and information move less efficiently than they should. Lean works well when everyone can see the problem, but no one has systematically cleaned up the process.
Lean is particularly suitable if daily life looks like this:
Many small interruptions create instability throughout the value stream.
Changeovers take too long because tools, instructions or responsibilities are not clarified.
An overview is missing in operations, and people spend time searching for the next correct step.
Lean is less effective when management believes the method is merely synonymous with cost-cutting or a faster pace. Without standard work and visible follow-up, Lean quickly ends up as boards with no effect.
When Six Sigma or TPM is the better choice
Six Sigma is relevant when the main problem is variation. If the same process yields different results and the company struggles with errors, deviations or unstable quality, more disciplined root-cause analysis is required. Here, cleaning up the flow is not enough. The process must be made more consistent.
TPM makes sense when equipment is a significant source of loss. This is especially true when production depends on a few critical machines, or when maintenance and operations work too far apart. TPM creates shared responsibility for the condition of the equipment and makes maintenance a part of daily operations, not just a reaction to breakdowns.
A practical rule of thumb:
Method | Use it when | Avoid starting here if |
|---|---|---|
Lean | The flow is lagging and waste is visible in the process | The problem is primarily technical variation |
Six Sigma | Errors and deviations require systematic analysis | The team lacks basic standardisation |
TPM | Equipment losses and stoppages dominate daily life | The machines are not the central bottleneck |
Why tools must be gathered in one place
The method is only half the job. The other half is the system that keeps the improvement alive. Many companies lose momentum because SOPs, action plans, maintenance routines, board meeting minutes and improvement proposals reside in separate folders or applications.
This is where otherwise good initiatives fail. Not because the team chose the wrong method, but because the organisation did not have a single place where shared practices could reside. This is also the reason why working with process automation in practice should be linked to communication and documentation from the start. Automation without shared management simply creates confusion faster.
When the latest work instruction, the decision from the last improvement meeting and the training material cannot be found in the same place, deviations become almost inevitable.
What works is a unified digital hub. Not as extra administration, but as the platform where improvements are translated into daily practice.
From plan to action with a clear roadmap
Most things go wrong in the transition between idea and operations. The team agrees on the potential, but daily routines quickly take over. Therefore, the roadmap must be simple enough to survive contact with reality. The most sustainable model starts with a small pilot area, a clear owner and a rhythm for follow-up.
Start with a defined pilot
A packing station is a good example. Not because the area is particularly glamorous, but because the problems are often easy to spot. Materials are missing. Labelling varies. Changeovers are done differently from employee to employee. Quality control happens too late. Here, the team can test improvements without paralyzing the rest of the factory.
A useful roadmap for the pilot area might look like this:
Define the problem clearly. Choose one area, one process or one recurring point of friction.
Assemble a cross-functional team. Operator, team leader, technician and ideally a planning or quality representative.
Document the current practice. Not the desired process, but the actual one.
Decide on few changes at a time. Too many adjustments simultaneously make it impossible to see what works.
Follow up in a fixed cadence. Brief meetings with clear responsibility points beat long status meetings.
What does not work is the classic grand project where the entire factory is expected to be lifted at once. Then the roadmap quickly becomes a management document for leaders instead of a working tool for those who actually need to use it.
Make progress visible to everyone
Once the pilot project is underway, communication must be concrete. Employees rarely accept changes just because management has decided on them. They accept them when they can see the purpose, follow the progress and understand what is expected of them.
A digital project workspace is useful here because it brings together decisions, tasks, updates and instructions in the same interface. This reduces the classic uncertainty about where the current version is located and who last changed what.
When changes need to take effect on the shop floor, it also helps to think about the physical surroundings of the work. Light, line of sight and concentration affect error risk, training and overall calmness in the working environment. For office and planning areas close to production, it might be relevant to look at how to optimise your office's daylight as part of the overall workspace design.
Remove resistance by making changes concrete
Resistance is rarely about laziness. It is often about ambiguity, poor timing or previous projects that fizzled out. Therefore, management should not just communicate more. It must communicate better.
It makes a noticeable difference to be clear about three things:
What is changing from today. Not at a strategic level, but very concretely in the workflow.
Who supports the employees along the way. There must be named individuals, not vague project groups.
When something will be evaluated again. Temporary solutions must not be perceived as hidden permanent demands.
Celebrate small operational breakthroughs quickly. When a team sees that their change is actually recognised and maintained, ownership grows much faster.
This is also where many underestimate the importance of visible leadership. If improvement work only lives in slides and weekly emails, it dies during the shift's first busy week. If the team leader actively uses the material in daily follow-ups, the change begins to look like normal operations.
Measure your success with the right KPIs
If a company only measures output, it gets a distorted picture of its production. High activity can easily mask poor quality, unstable operations and growing rework. KPIs must therefore be chosen so that they show pace, quality and stability in the process alike.
The visual overview helps, but the numbers must always be linked to action in local operations.
Measure what drives behaviour
OEE is useful because it aggregates a large part of the equipment perspective into a single key figure. In the research material, OEE is described as a measure of the machine's or system's utilisation rate and, thus, how efficient production is. It is used for the entire production, for lines or for individual systems, as described by VS Automatic on production optimisation and OEE.
But OEE cannot stand alone. A line can look reasonable in terms of equipment efficiency while simultaneously passing errors forward or creating queues before the next process step. Therefore, the KPI set should also include aspects such as cycle time, First Pass Yield, lead time and cost per unit produced, described qualitatively and understood in a local context.
A good practice is to ask: If this KPI improves, will the floor work smarter or just faster? If the answer is faster, the goal is likely too narrow.
Make KPIs operational
KPIs only work when those close to the process can react to them. This requires simple presentation and quick access. A report that arrives long after the shift does not help the operator, team leader or technician.
Therefore, digital information screens work better in many environments than traditional monthly reports. They create a shared picture of operations here and now, making deviations visible while they can still be addressed.
Consider this structure:
KPI type | Who uses it | What it should trigger |
|---|---|---|
Daily operational goals | Operators and team leaders | Quick reaction to deviations |
Weekly follow-up | Production management and support functions | Prioritisation of improvements |
Management overview | Factory manager and cross-functional leadership | Resource decisions and direction |
Use the qualitative signals as well
Raw numbers do not tell the whole story. Comments from employees, descriptions of recurring irritations and suggestions from shift meetings often contain the root causes behind the deviations. If many report that the same machine is difficult to set up, or that the same instruction is misunderstood, it is a strong signal, even without an advanced analysis model.
Here, AI can be useful. Not as a replacement for leadership, but as an aid to sort patterns in large volumes of feedback, group themes and point to recurring issues. This requires, however, that the input is stored collectively in a digital format rather than scattered across emails, paper notes and local files.
The best KPI systems combine visible operational figures with the employees' own observations. Only then does the measurement become useful for management.
How to anchor improvements in the culture
The real test comes after the pilot project. Not when the improvement is launched, but when it must survive holidays, busy periods, staff turnover and new priorities. If the change only resides within the project group, it disappears. If it becomes part of the standard, the culture and the shared knowledge, it remains.
The long-term work can be thought of as a chain of a few, fixed steps.
Standardisation is what makes improvements sustainable
Many talk about culture but skip standardisation. That is a mistake. An improvement only becomes real when it is translated into a clear work instruction, a known routine and an expected practice across teams.
This does not mean rigid bureaucracy. It means that the company decides what the new best-known method is and makes it easily accessible. If Team A finds a smarter way to do a changeover, Team B and C should not have to reinvent it.
Three elements make the work stronger:
An updated library of work instructions that people can actually find.
Training material close to the task in the form of short guides, visual steps or video.
Clear owners of the standards so documents do not drift without accountability.
Knowledge sharing must be part of operations
Anchoring does not happen through campaigns. It happens through repetition and access. When improvement suggestions, SOPs, error lessons and local solutions are consolidated in a searchable knowledge base, it becomes much easier to lift the organisation as a whole.
This is also where management should work consciously with change as a discipline. Good changes do not automatically slide into daily routines. They must be supported, followed up on and made meaningful. Working with change management and change models is therefore closely linked to lasting production optimisation, even though many mistakenly treat it as an HR track.
A healthy improvement culture can often be recognised by these signs:
Employees share problems early because they expect action rather than blame.
New solutions are documented quickly so that learning does not remain local and temporary.
Management follows up consistently, even when pressure increases elsewhere in the organisation.
AI only makes a difference when the foundation is in place
AI can significantly strengthen knowledge sharing. An intelligent search function can help employees find instructions, previous solutions and relevant context faster than a traditional folder structure. But technology does not salvage a mess. If the content is outdated, contradictory or scattered, the search will simply find chaos faster.
Therefore, the best investment is often not another isolated improvement tool, but a strong system for shared knowledge. When the company builds that foundation properly, AI becomes a practical layer on top. Not a fancy layer without substance.
This is how improvements last. Not because the organisation talks more about learning, but because it makes learning a concrete part of work every day.
If work with production optimisation is to hold up across shifts, locations and professional groups, it requires more than just choosing a method. It requires a place where communication, SOPs, improvement initiatives, information screens and searchable knowledge connect. Colibo is developed for precisely that type of complex organisation and can bring together internal communication, knowledge sharing and AI-supported access to operational knowledge in one platform.